Cov ntsiab lus tseem ceeb ntawm GMT Automotive Moulding Tooling
Sep 09, 2026
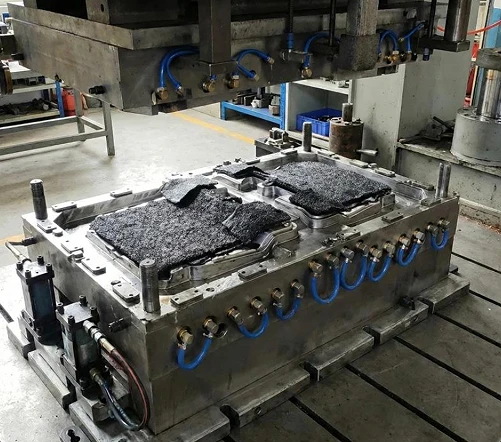
Thermoplastic GMT iav fiber ntau lev-cov khoom siv ntxiv, nrog rau lawv cov txiaj ntsig zoo ntawm lub teeb yuag, kev cuam tshuam, thiab rov ua dua tshiab, tau siv dav hauv cov khoom siv loj rau cov tsheb tshiab, xws li roj teeb tiv thaiv, hauv qab lub cev tiv thaiv, thiab pem hauv ntej -end modules. Tsis zoo li cov txheej txheem thermoset SMC compression molding txheej txheem, GMT molding siv cov txheej txheem txheej txheem nrog rau sab nraud preheating ntawm cov ntaub ntawv thiab pwm txias rau shaping, uas imposes tshwj xeeb yuav tsum tau rau cov cuab yeej rigidity, kub tswj systems, shear lug, thiab automation compatibility. Daim ntawv no tsom mus rau lub tsheb loj GMT cov khoom thiab nthuav qhia cov qauv tsim ntawm cov cuab yeej thermoplastic molding, cov ntsiab lus tseem ceeb ntawm kev tswj qhov kub thiab txias, cov teeb meem tshwm sim, thiab cov txheej txheem kev txhim kho zoo sib xws.
I. Zuag qhia tag nrho cov qauv ntawm kev ua hauj lwm fixture (cov tsheb loj loj)
1. Formwork ncej lub cev
Khoom siv: P20 / 718H hardened steel nrog HRC{2}} hardness. Thickened thav duab thiab rov qab qhov cuab lub zog ribs kom tiv taus 10 - 20 MPa siab siab thiab tiv thaiv loj - pwm pwm los ntawm deforming vim lub siab.
Pwm kab noj hniav nto yog polished nrog Ra0.8 - 1.6 μm; lub kaum sab xis yog 3℃- 5℃los tiv thaiv nto khawb thaum demolding ntawm qhov loj; precision qhia pins thiab coj lub tes tsho + positioning pins los tswj lub kaw qhov sib txawv thiab suppress flash.
Shearing ntug: Stretchable ntsug shearing ntug qauv, ncaj shearing hauv pwm, txo cov txheej txheem trimming tom ntej thiab tswj lub thickness ntawm lub teeb.
· Ejection system: Multi-point synchronous ejection, tiv thaiv warping thaum ejection ntawm loj- qhov loj me; tuaj yeem ua ke nrog lub tshuab nqus tsev kom txhim kho qhov zoo.
2. Thermal tswj system [Lub ntsiab ntawm GMT tooling]
Qhov sib txawv tseem ceeb ntawm GMT thiab SMC: SMC pwm tau ua kom sov tsis tu ncua; GMT ua hauj lwm fixtures yog rau txias.
1. Partitioned siab- ntws tob- qhov dej txias Circuit Court (tseem ceeb rau qhov loj)
Rau cov khoom loj tshaj li ib 'meter' loj, qhov sib txawv ntawm qhov sib txawv ntawm cov phab ntsa thicknesses thiab rib txoj haujlwm tuaj yeem yooj yim ua rau muaj kev ntxhov siab thiab warping deformation; siv cov kev tswj qhov kub thiab txias, cov cheeb tsam tseem ceeb tuaj yeem ua rau ua kom txias txias, ua kom muaj cua sov sib npaug, thiab ua kom muaj kev ruaj ntseg.
1. Cov cua sov hauv zos: Cov cua kub cua sov tuaj yeem teeb tsa hauv qhov chaw nruab nrab ntawm qhov chaw nruab nrab thiab cov tav tuab tuab kom tsis txhob muaj cua txias thiab cov khoom tsis txaus.
Pwm ua haujlwm kub: 60 - 90℃; Preheating sab nraum cov ntaub ntawv rauv: 170 - 190 degree, nruj me ntsis txwv tsis pub tshaj 230 degree, tiv thaiv degradation ntawm PP matrix.
3. Automated adaptation interface
· Reserved khoom tuav interface rau cov neeg kho tshuab tes thiab daim ntawv tso cai txwv blocks;
· Integrated roj Circuit Court thiab cua Circuit Court; tau tshaj hydraulic xovxwm tonnage: 1600 - 4000t loj hydraulic xovxwm.
II. Cov yam ntxwv tseem ceeb ntawm Hom Automotive GMT Cheebtsam thiab Tooling
|
GMT qhov chaw |
Cov ntsiab lus tseem ceeb ntawm kev tsim cov khaub ncaws ua haujlwm |
|
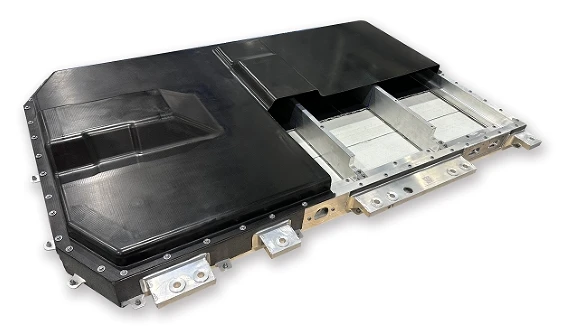
Roj teeb pob tiv thaiv npog |
Loj- thaj tsam tiaj tus phaj + ntom ntom ntom ntom ntom ntu; tsam txias; siab rigidity pwm ncej; ntau protrusions rau installation; hauv -pwm trimming |
|
Tsheb underbody guard phaj |
High nam piv, nyias phab ntsa; tswj warping; nqus tsev vacuum; qis flange |
|
Pem hauv ntej -end module bracket |
Ntau qhov embedded; complex concavities thiab convexities; tswj cov ntaub ntawv ntws, tiv thaiv fibers los ntawm ntau shearing |
|
anti-kev sib tsoo beam |
Thick -section structural Cheebtsam; Kev tuav tswj kom txaus; Ntsuas cua txias kom ntseeg tau tias muaj kev cuam tshuam kev ua haujlwm |
III. Qhov txawv ntawm GMT Tooling thiab SMC Tooling
|
qhov project |
Thermoplastic GMT cuab yeej |
Thermosetting SMC cuab yeej |
|
Moulding txoj cai |
Cov ntaub ntawv yog preheated sab nraum lub qhov cub, thiab cov pwm txias thiab solidifies (lub cev hloov theem) |
Cov pwm tau ua kom sov tsis tu ncua, thiab cov resin raug kho tshuaj thiab hla -txuas. |
|
kub tswj qhov system |
Feem ntau yog siv cov cua txias |
Cov cua kub tsis tu ncua (kub roj / hluav taws xob cua sov) |
|
molding voj voog |
45-90 s |
3-6 feeb |
|
cov khoom siv rov ua dua tshiab |
Cov khoom yuav raug crushed thiab rov siv dua. |
unrecyclable |
|
Kev pheej hmoo ua tsis tiav |
Lub caij txias thiab kub lub voj voog qaug zog, kev thaiv dej, hniav ntug hnav |
Siab -kub oxidation corrosion |
IV. Feem ntau ua tsis tiav ntawm Loj - teev GMT Cov Cuab Yeej & Tsim Kev Tiv Thaiv Kev Ntsuas
Part warping, dimension sib txawv:Lub hauv paus ua rau tsis sib xws; cov kev daws teeb meem: faib cov cua txias, zoo li cov dej raws, kev ua kom zoo ntawm phab ntsa thickness sib txawv, tsim nyog pub rau shrinkage.
Kev tsis sib haum xeeb hauv fiber ntau thiab tsis muaj zog hauv zos:Kev txwv ntawm cov khoom siv raw; Segmented tswj ntawm pwm kaw ceev kom tiv thaiv fibers los ntawm raug hnyav heev ntxuav thiab tshem tawm.
Tshaj ya ntug:Txhim khu lub rigidity ntawm pwm ncej; txhim kho qhov chaw raug ntawm cov kab lus qhia; optimize qhov sib txawv ntawm cov hniav shearing
.Nthuav ntug sai heev hnav:Local quenching hardening ntawm txiav ntug.
Kev kho deformation:Ua ntau yam synchronous extrusion thiab teeb tsa lub kaum sab xis tsim nyog rau pwm.
V. Ua kom tiav GMT Moulding txheej txheem ntws
Txiav ntawm GMT cov ntaub ntawv → Preheating hauv qhov cub cua kub ntawm 170 - 190℃→ Tsis siv neeg txhais tes sai sai pub cov khoom mus rau hauv lub workpiece kab noj hniav → ceev ceev kaw ntawm hydraulic xovxwm → High- siab tuav (10 - 20 MPa) → Txias thiab shaping hauv pwm → Internal shearing thiab trimming → nkag mus rau hauv cov khoom sib txuas thiab sib txuas ntxiv lub voj voog.