


Carbon Fiber Cav Hood Pwm
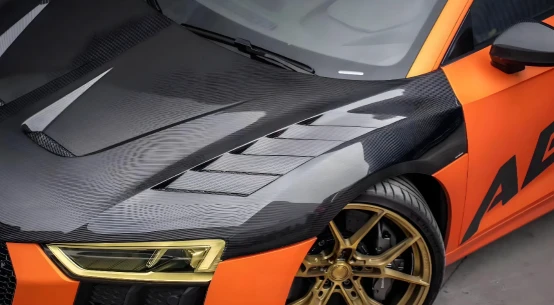
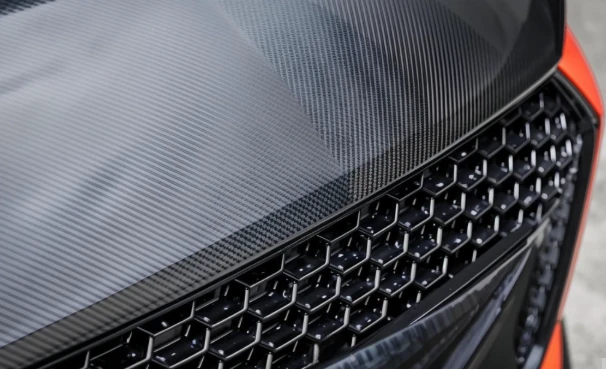
Cov pa roj carbon fiber hood pwm yog cov cuab yeej tshwj xeeb siv los tsim cov pa roj carbon fiber hood (CFRP Hood) ntawm tsheb. Cov ntsiab lus tseem ceeb yog qhov siab precision, siab rigidity, thiab qis thermal deformation los xyuas kom meej qhov tsos, qhov tseeb qhov tseeb, thiab lub zog ntawm lub hood ....
- Kev xa khoom sai
- Quality Assurance
- 24/7 Kev Pabcuam Cov Neeg Siv Khoom
Khoom Taw qhia
Cov pa roj carbon fiber hood pwm yog cov cuab yeej tshwj xeeb siv los tsim cov pa roj carbon fiber hood (CFRP Hood) ntawm tsheb. Cov ntsiab lus tseem ceeb yog qhov siab precision, siab rigidity, thiab qis thermal deformation los xyuas kom meej qhov tsos, qhov tseeb qhov tseeb, thiab lub zog ntawm lub hood.
I. Kev xaiv cov khoom siv pwm
·Aluminium alloy (xws li 6061-T6):Lub teeb yuag, ceev kub conductivity, ua haujlwm zoo, haum rau me me thiab nruab nrab batch ntau lawm thiab sai prototyping.
·Hlau (xws li P20, S50C):Lub zog siab, zoo hnav tsis kam, haum rau kev tsim khoom loj, tab sis hnyav hnyav thiab tus nqi siab.
·Cov khoom siv carbon fiber ntau (CFRP):Tsawg thermal expansion coefficient, zoo compatibility nrog cov khoom, lub teeb yuag, haum rau siab -precision thiab complex nkhaus nto pwm, tab sis tus nqi siab.
II. Cov ntsiab lus tseem ceeb ntawm Mould Structure Design
1.Pwm faib tsim
- Cov qauv siv lub puab thiab sab nrauv pwm cais tsim. Txoj kab sib faib yog nyob rau ntawm qhov tsis yog - qhov tshwm sim ntawm lub hood (xws li thaj tsam ntawm ntug flange), kom ntseeg tau tias muaj qhov ua tiav thiab du demolding.
- Tsim tauflange ntug moduleenables ob qho tib si molding thiab ntug txiav.
2.Profile thiab Precision
- Raws li 3D scanning cov ntaub ntawv ntawm tag nrho lub tsheb, tus qauv yog ua los xyuas kom meej qhov tseeb ntawm haum nrog lub tsheb lub cev.
- Qhov saum npoo ntawm qhov profile yuav tsum tau mus txog qib A (Ra Tsawg dua lossis sib npaug ntawm 0.8 μm), uas ncaj qha txiav txim siab qhov zoo ntawm cov khoom.
- Qhov ntev ntawm qhov tseem ceeb yog tswj nyob rau hauv ib tug kam rau ua ntawm ± 0.3 hli, thiab lub installation qhov yog precisely positioned.
3. Kev txhawb zog thiab kev txhawb nqa
- Sab nraub qaum ntawm cov pwm yog nruab nrog kab sib chaws-zoo li cov hlua txuas ntxiv (qhov sib nrug ntawm 300-500 mm), uas tsis yog tsuas yog txo qhov hnyav xwb tab sis kuj txhim kho kev nruj thiab tiv thaiv kev deformation nyob rau hauv siab.
- Cov ncej txhawb nqa yuav tsum nyob ze rau ntawm qhov chaw pwm, sib npaug sib faib lub siab thiab tsis txhob muaj kev ntxhov siab hauv zos.
4.Qhov cua thiab lub tshuab nqus tsev vacuum
- Qhov cua grooves yog teem rau ntawm cov npoo ntawm cov pwm kab noj hniav (dav 0.5-1.0 mm), tiv thaiv cov huab cua tsis zoo los ntawm kev ua rau lub ntsej muag blemishes lossis cov khoom tsis txaus.
- Nws yog ib qho tsim nyog yuav tsum tau sib xws nrog lub tshuab nqus tsev / kub xovxwm tank txheej txheem. Cov pwm yuav tsum muaj qhov zoo ntawm lub tshuab nqus tsev sealing kev ua tau zoo (txo qis dua lossis sib npaug ntawm 0.01 Pa・m³ / s).

III. Adaptation ntawm Mainstream Manufacturing txheej txheem
RTM (Resin Hloov Molding): Cov pwm yuav tsum muaj kev nruj nruj thiab yuav tsum muaj kev sib khi zoo. Nws haum rau nruab nrab - ntim thiab siab - cov khoom zoo.
autoclave molding: Cov pwm yuav tsum tiv taus qhov kub thiab txias (120-180 degree) thiab siab siab (0.5-1.0 MPa), thiab muaj cov kev xav tau siab heev rau thermal stability.
Nqus hnab molding: Tus nqi qis, haum rau me me batch ntau lawm los yog sim khiav, tab sis nws muaj qhov yuav tsum tau ua rau saum npoo ntawm pwm thiab sealing kev ua tau zoo.
Expansion core pwm txheej txheem: Siv cov ntaub ntawv nthuav dav (xws li Koridion), nws tuaj yeemCov txheej txheem nyuaj ntawm lub cev - ua duct nrog lub qhov cua channel, Tsis tas yuav tsum muaj kev sib txuas ntxiv, thiab lub voj voog molding yog luv (kwv yees li 8-15 feeb).
IV. Cov lus ceeb toom tseem ceeb rau kev tsim khoom thiab kev siv
Hloov cov ces kaum thiab kev hloov pauv: Kab noj hniav ces kaum, hauv paus ntawm rib filletR Loj dua lossis sib npaug li 3 hli, Thickness hloov pauv gradient (qhov sib piv Tsawg dua lossis sib npaug li 1: 5), kom tsis txhob muaj kev ntxhov siab thiab kho warping.
Cua sov / cua txias system: Ua- nyob rau hauv cov kav dej kub cua sov kom ntseeg tau tias qhov kub ntawm qhov sib txawv thaum kho yog Tsawg dua lossis sib npaug li ± 5 degree, tiv thaiv kev ntxhov siab hauv cov khoom.
Demolding thiab Maintenance:Siv tshwj xeeb siab -kub- resistant tso tawm; tom qab molding, maj mam txias thiab tshem tawm cov pwm tusyees kom tsis txhob warping; tsis tu ncua xyuas qhov tseeb ntawm qhov chaw thiab sealing kev ua tau zoo.

V. Tej yam tsis xws luag thiab Countermeasures
Nto npuas / pinholes: Txhim kho qhov kev ua tau zoo, txhim kho lub tshuab nqus tsev, thiab ua kom zoo dua cov dej ntws.
Cov khoom sib txawv thiab deformation: Optimize lub rigidity ntawm pwm, tswj tus nqi cua txias, thiab kho cov kev taw qhia ntawm lub fiber layup.
Pwm kab misalignment: Txhim kho cov pwm qhov chaw thiab txhim kho pwm kaw qhov tseeb.
Txheej txheej: Xyuas kom meej tias lub laminate tsis muaj wrinkles, uas lub tshuab nqus tsev compaction yog tag nrho, thiab cov curing tsis tsim nyog.
Cim npe nrov: Tuam Tshoj carbon fiber cav hood pwm manufacturers, hoobkas


